
Reliable, Accurate, Fast and Highly Versatile Checkweighing Solutions – Xact offer flexible checkweighing solutions helping you to achieve 100% product quality
Xact’s box checkweighers are purpose-built to weigh cartons, cases, and boxed products at the end of your production or packaging line, ensuring every shipment meets your exact specifications. Our systems verify that each box contains the correct quantity of product, helping you prevent underfilled deliveries and avoid unnecessary product giveaway.
Whether you’re packing food, pharmaceuticals, or industrial goods, Xact’s range of box checkweighers delivers the precision, speed, and reliability you need to maintain quality and protect your bottom line.
Our range starts from £8,000
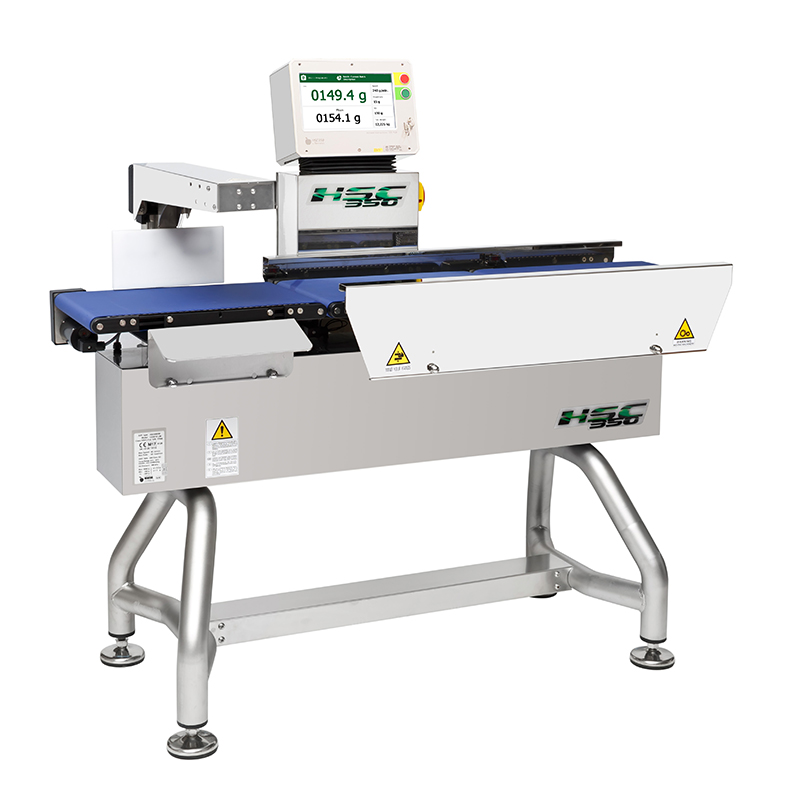
C Series Checkweigher
A ‘Tailor-Made Solution’ – Compact, Modular and Cost Effective
The HSC350 C Series checkweigher is our standard machine suitable for all types of products. This is the compact, modular and cost-effective solution that integrates into the production line when space is at a premium. The sturdy machine is flexible which means a Metal Detector with display and labelling systems can easily be fitted and thanks to its flat, easily accessible surfaces, the C Series is easily cleaned and sanitised.

Aerosols

Cans

Chemicals

Cosmetics

Food

Non-Food

Pharma
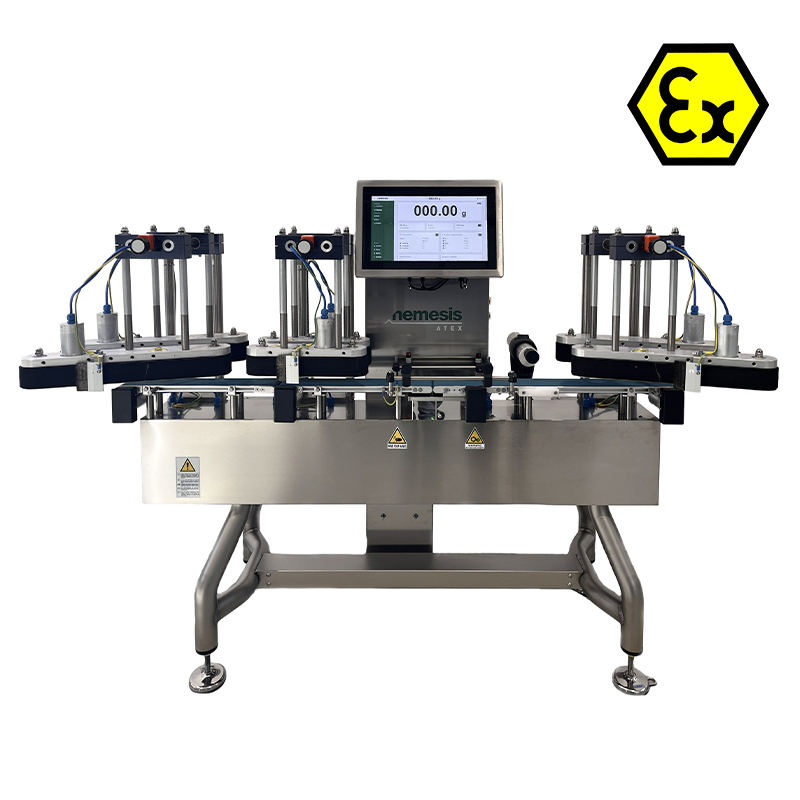
ATEX – Certified Machines for Hazardous (Explosive) Areas
Weighing solutions for explosive atmospheres due to the presence of flammable gases, vapours, or dusts
The system features complete electrical bonding and grounding, preventing electrical discharge and eliminating the risk of dangerous spark generation. Designed and manufactured in compliance with the specific requirements of the regulations for ATEX Zone 2/22, these checkweighers can be installed close to high explosion-risk processes, such as aerosol can filling while ensuring excellent weighing performance and meeting the highest safety standards.

LUMINA Series
A Revolution in the Range – The True Cross-Device Control Experience
The first truly multimedia checkweigher, with commands that can be remotely controlled from a smartphone, tablet, or PC. The completely redesigned control interface is operated through an innovative 15-inch vertically oriented touchscreen panel which is a unique feature in the market. The interface can also be mirrored to other devices, allowing operators to set programs, start or stop the machine, and monitor statistics and reports from anywhere, even remotely.

G Series Checkweigher
Washable For Harsh Environments – Innovative, Hygienic, Cost Effective
The G Series checkweigher is ideally suited for bulk meat, fish and cheese. This range is specifically designed for harsh environments and bulk product applications, where cleaning and sanitising play a major role. With an IP66, easy-to-disassemble conveyor’s structure the G Series is easy to clean and with a 100% stainless steel frame, these systems are the ideal solution for the food processing industry.
Chemicals
Cans

Jars

Bricks

Cheese

Fish

Meat


R Series Checkweigher
Ultra Fast and Harsh Environments
The HSC350 ‘R Series’ is a sturdy chain checkweigher for extreme environments. With high accuracy, innovative design for any application in a harsh industrial environment. Available in numerous configurations, the protected motors and open design makes cleaning easy and hygiene is maintained.
Aerosols
Cans
Chemicals
Cosmetics
Food
Bricks

Bottling

S Series Checkweigher
Pharmaceutical/Medical Industry – Light Weight, High Speed
The S series includes is a high speed checkweigher designed for small packages. It’s modular checkweighers that meet the current requirements of the pharmaceutical industry, in particular the GMP regulations and the stringent quality control regulations.
Aerosols
Chemicals
Cosmetics
Pharma
Non-Food

MX Series Metal Detector
Combined Checkweigher and Metal Detector
For a total end-of-line inspection system the MX Series is designed for reduced spaces to simultaneously weigh and find contaminants. It complies with HACCP and GMP quality standards and is available in multi-frequency and multi-spectrum versions.


Case Study
Weighing and Grading Line in 8 Product Categories with 16 Outlets
A European food processor specialising in fresh and dried fruit required a weighing and grading solution capable of handling large volumes of chestnuts.
We achieved:

Box checkweighers are widely used in industries such as:
By automatically inspecting carton weights in real time, our checkweighers detect issues such as missing items, incorrect pack counts, or packaging errors before they leave your facility. Xact’s dynamic checkweighers operate without interrupting conveyor flow, rejecting any boxes that fall outside your defined weight range.
Key considerations when selecting a box checkweigher include the maximum product weight, carton dimensions, production line speed and integration with other inspection technologies.

Features of Box Checkweighers
Different types of box checkweighers are designed to handle various product sizes, throughput requirements and industrial environments.
Heavy-Duty Box Checkweighers
Heavy-duty systems are designed for large or heavy cartons, often weighing tens of kilograms. These checkweighers typically feature reinforced frames and larger conveyor belts to support heavy loads.
Typical applications include:
- Bulk food cartons
- Logistics and shipping cases
- Industrial parts packaging
- Large consumer goods shipments
Some box checkweighers are capable of handling weights of up to around 60kg, making them ideal for heavy carton inspection at the end of packaging lines.
Compact Carton Checkweighers
Not all boxed products are large. Many industries require systems capable of inspecting small to medium cartons such as pharmaceutical boxes, food cartons or cosmetics packaging.
Compact box checkweighers are commonly used for:
- Packaged food cartons
- Pharmaceutical secondary packaging
- Cosmetic and personal care products
- Household goods and retail packaging
These systems provide high accuracy while maintaining a compact footprint within the production line.
Inline Carton Inspection Systems
Most box checkweighers operate as inline dynamic weighing systems, allowing every box to be weighed while production continues at full speed. This ensures 100% inspection without slowing the packaging process.
In addition to weight verification, these systems may also:
- Detect missing items inside cartons
- Classify products by weight
- Generate production data for quality control
Dynamic carton weighing is commonly used in many industries to ensure packaging consistency and reliability before products are shipped.
Key Features to Consider
Choosing the right box checkweigher requires evaluating both production requirements and machine capabilities.
How to Choose the Right Box Checkweigher
Choosing a box checkweigher isn’t just about weight range. It needs to suit your product, keep up with your line speed, and work alongside the rest of your equipment without causing bottlenecks.
Our checkweighing systems help producers and packaging operations find the right fit for their setup. Rather than a one-size-fits-all approach, the focus is on understanding how your line runs and recommending equipment that will perform reliably in that environment.
Each system is specified with your production in mind, from throughput and accuracy requirements through to how it integrates with existing processes. That upfront work helps avoid common issues like underperforming equipment or unnecessary downtime.
Support doesn’t stop at supply. Xact works with customers to make sure systems are correctly specified from the outset and continues to provide guidance as production needs evolve.
The goal is simple: a checkweighing solution that fits your line properly and keeps things moving.

